Setups Documented And Retained
Programs, tooling and fixturing are stored, so repeat orders reproduce the part that was approved rather than a fresh interpretation of it.
To fabricate parts and assemblies that fit and function first time, by reviewing designs for manufacturability honestly before anything is cut or quoted.
Who We Are
MCB Smide & Maskin is a contract sheet metal fabricator producing enclosures, cabinets, chassis, panels, brackets, ducting and welded assemblies for electronics, machine building, food equipment, ventilation, architectural and transport customers. Capability covers laser cutting and punching, CNC press brake forming, rolling, welding in steel, stainless and aluminum, hardware insertion, machining of fabricated parts, assembly and finishing including powder coating, plating, graining and passivation. We work from prototype through to repeat production, and we review every new part for manufacturability before quoting, since the great majority of fabrication problems originate in the design rather than in the shop.
The design issues are consistent and easily fixed early: insufficient bend relief causing tearing at flange corners, flanges too short to form against the tooling, holes placed too close to a bend line and distorting during forming, tolerance stacks that no realistic forming process can meet, and welded assemblies specified without accounting for heat distortion. MCB Smide & Maskin raises each of these at quotation with a suggested alternative rather than quoting as drawn and dealing with it later. Forming accuracy also depends on allowing correctly for springback, which differs by alloy and temper even at identical thickness, so we form test pieces when working with an unfamiliar material rather than assuming.
Compliance
Pre-treatment before coating is controlled and documented.
Drawings reviewed for manufacturability before anything is cut
Track Record
Our Mission
To deliver finished, assembled work ready for the customer\'s next step, rather than components that still require several operations elsewhere.
Sectors
Food equipment makers need hygienic welding and finishing to their own standards.
Client Feedback
Their design review changed four features before we committed. Two of those would have torn at the bend corners and we would have found out at first article.
The enclosure fit is consistent batch to batch, which it never was before. They explained it was weld fixturing and sequence, not the forming.
We had chased coating adhesion failures across two suppliers. They identified pre-treatment in the first conversation and it has not recurred since.
MCB Smide & Maskin will review your parts for manufacturability, suggest alternatives where needed, and quote with realistic tolerances.
Forming accuracy depends on bend sequence, tooling selection and correct allowance for material springback, which varies by alloy and temper even at identical thickness.
Our Advantages
Programs, tooling and fixturing are stored, so repeat orders reproduce the part that was approved rather than a fresh interpretation of it.
Fixturing and weld sequence are planned for heat management, because distortion in a welded enclosure shows up immediately as door and panel misfit.
Hardware, gaskets, locks and labeling are fitted and checked, so you receive usable assemblies rather than parts needing further operations.
Bend relief, flange length, hole proximity and tolerance achievability are checked at quotation, with alternatives suggested rather than problems deferred.
Surface preparation is specified and verified, since almost every powder coating failure originates in pre-treatment rather than in the coating itself.
Forming allowance is set by alloy and temper, and we form test pieces on unfamiliar material instead of assuming a generic figure.
Bend allowances are calculated per material and thickness rather than dialed in by eye, which is what keeps formed parts within drawing tolerance.
Cleaning and pre-treatment stages before powder coating are process controlled and recorded, since adhesion failures are always a preparation failure.
We flag bend reliefs, tolerance stacks, hardware clearances and features that drive cost, so a small drawing change can save a great deal of money.
Our Services
Laser cutting and CNC punching of blanks with forming features, louvers, embossments, countersinks and hardware preparation, nested for material yield. Punched forming features are often more economical than secondary operations where quantities justify the tooling.
Request a Quote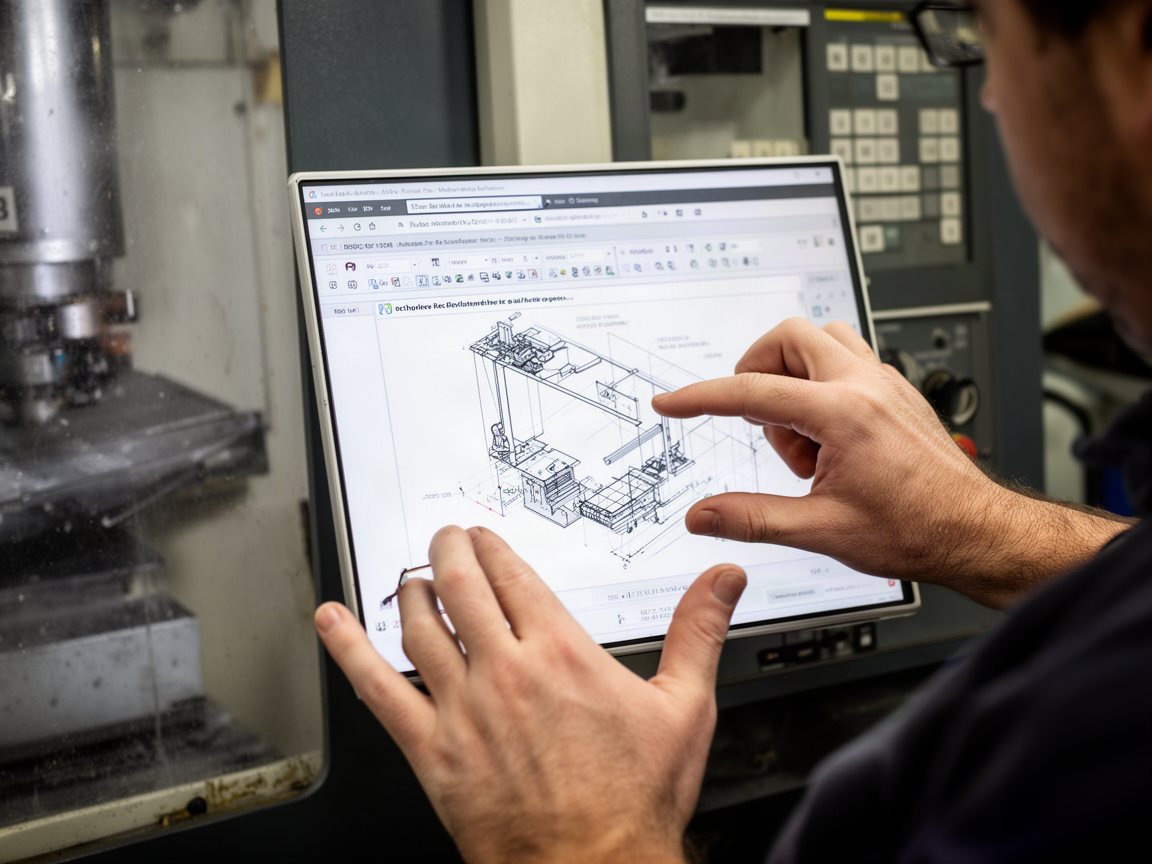
Insertion of self-clinching nuts, studs and standoffs, plus tapping, counterboring, reaming and machining of fabricated parts where tolerance requires it. Hardware insertion is specified against sheet thickness and material, since pull-out and torque performance depend on correct selection.
Request a Quote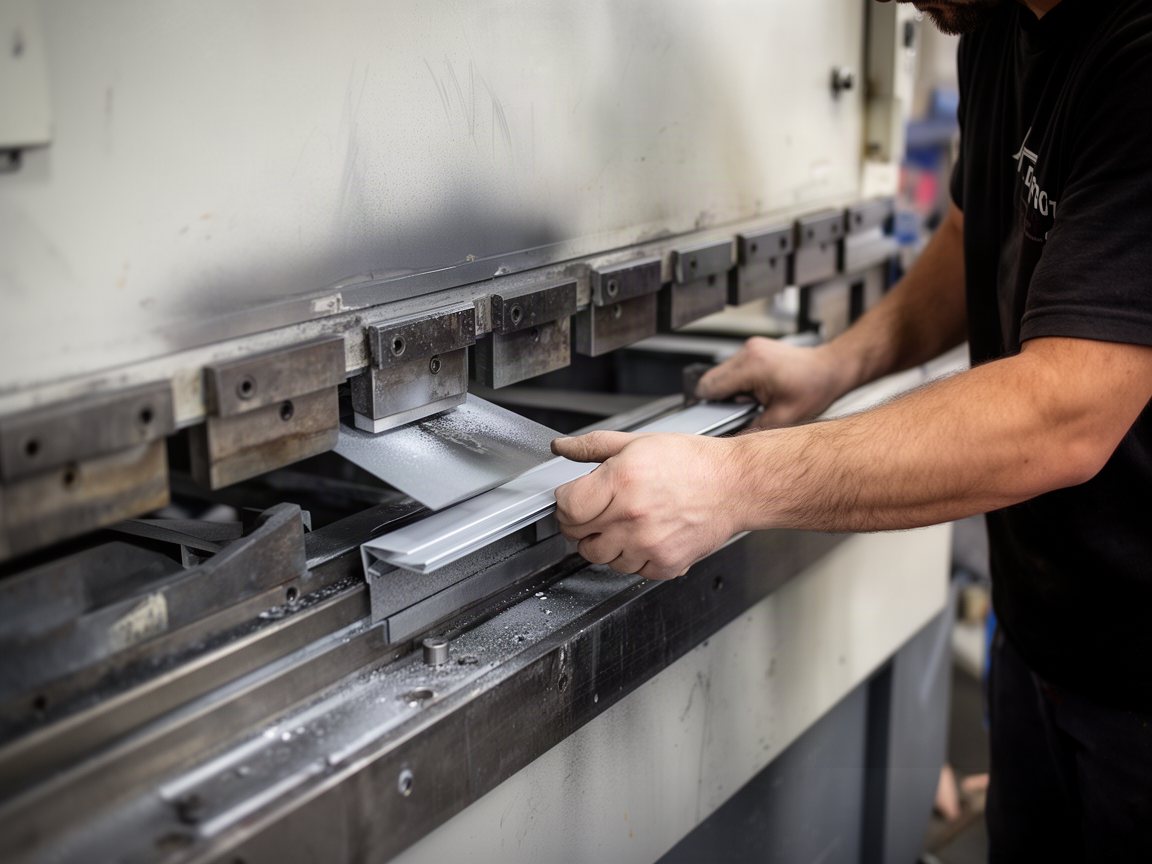
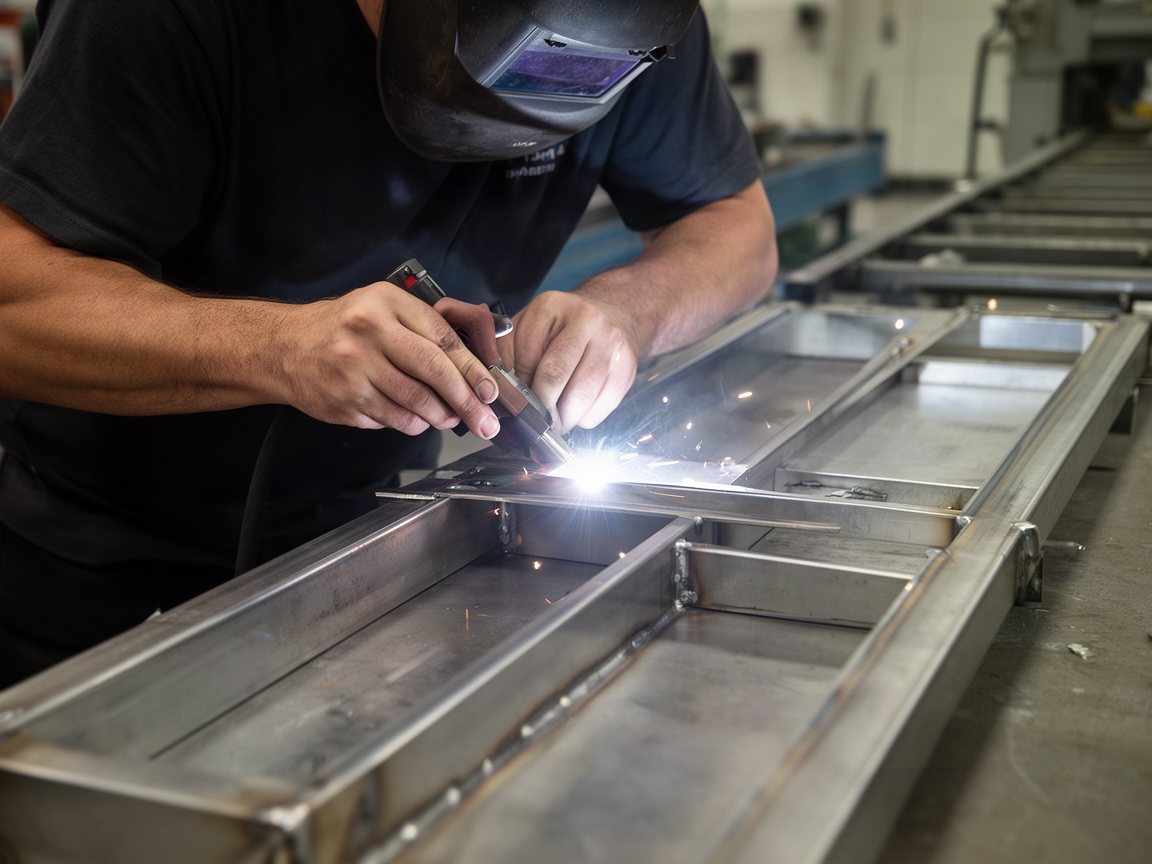
Welding in mild steel, stainless and aluminum covering spot, stud, TIG and MIG processes, with fixturing to control distortion and weld sequences planned for heat management. Welded enclosures receive particular attention to flatness and squareness, since distortion there affects door and panel fit directly.
Request a Quote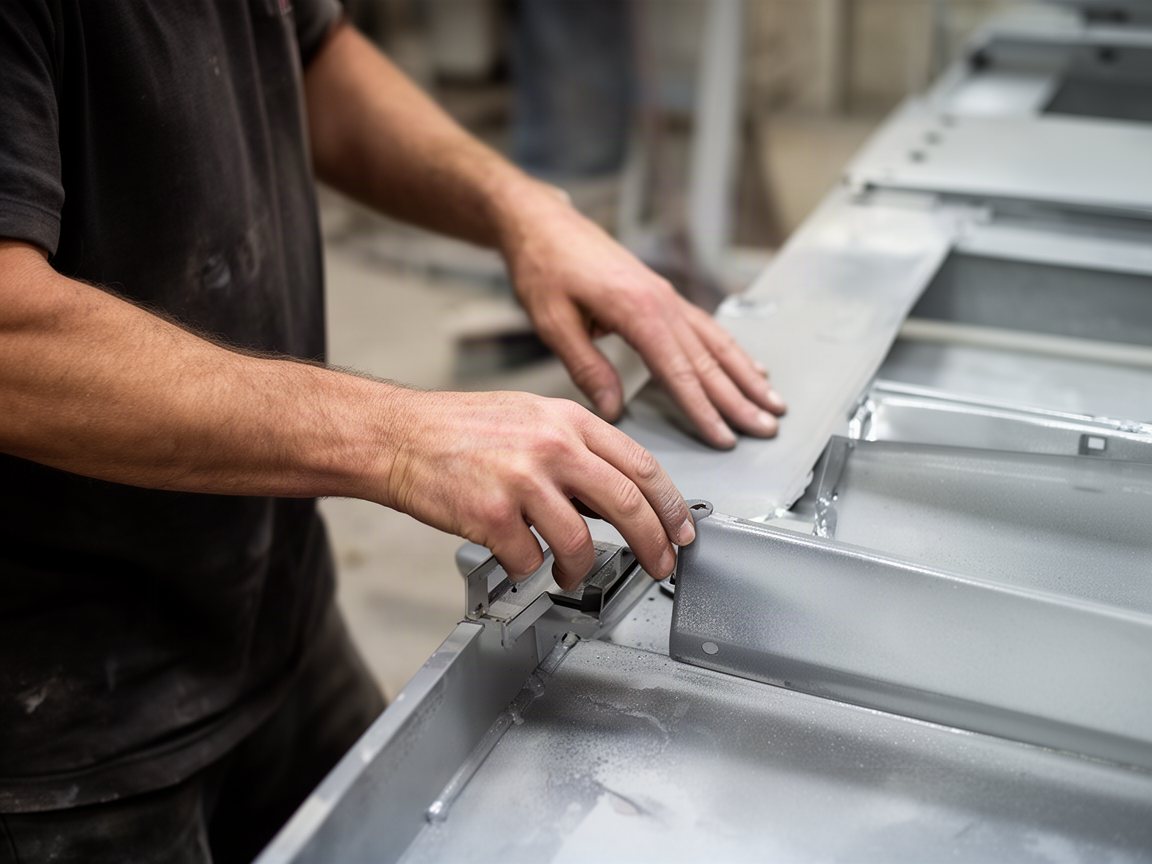
Review of new parts before quoting, covering bend relief, minimum flange length against available tooling, hole-to-bend proximity, tolerance achievability, nesting efficiency and weld distortion risk. Issues come with suggested alternatives, since most are resolved by a small change at design stage and are expensive to resolve afterward.
Request a Quote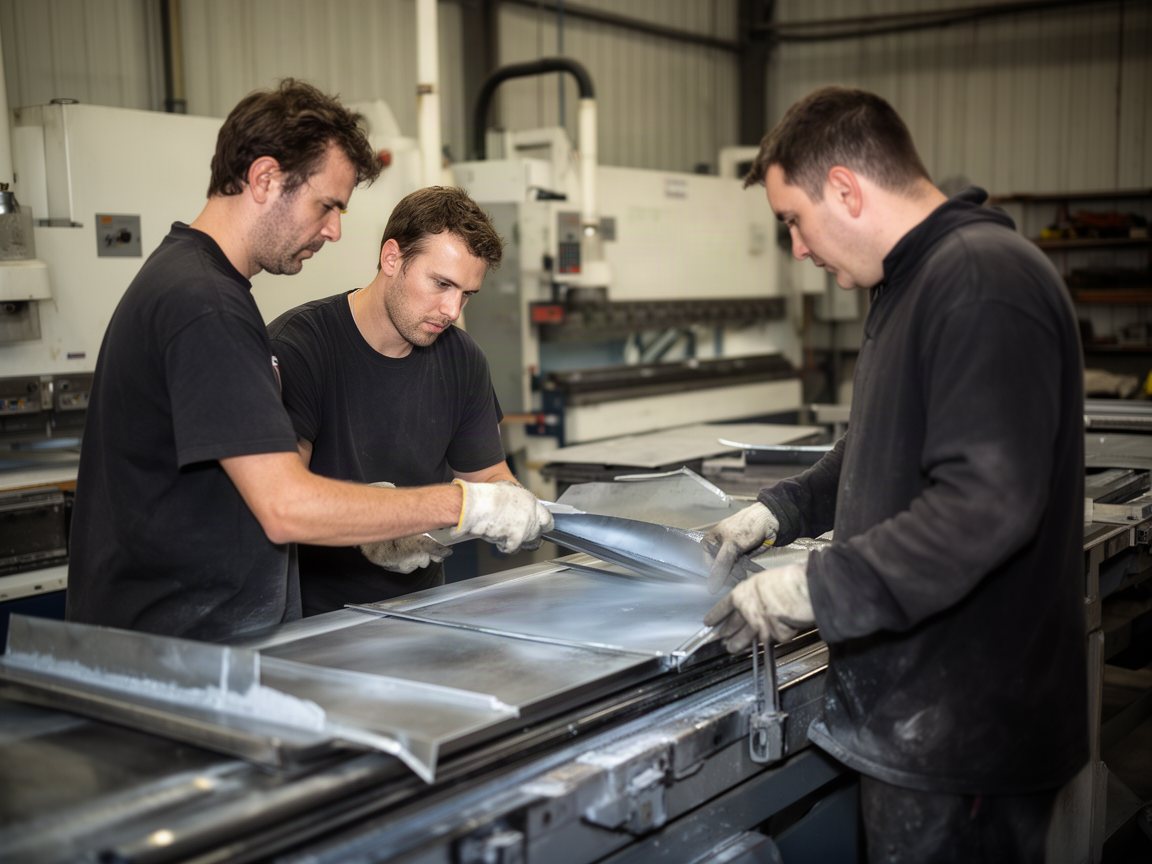
Sub-assembly and full assembly including hardware, gaskets, insulation, locks, hinges, labeling, wiring harness installation and functional checks, delivered ready to use. Taking assembly in-house removes handling, transport and coordination steps that frequently cost more than the assembly labor itself.
Request a Quote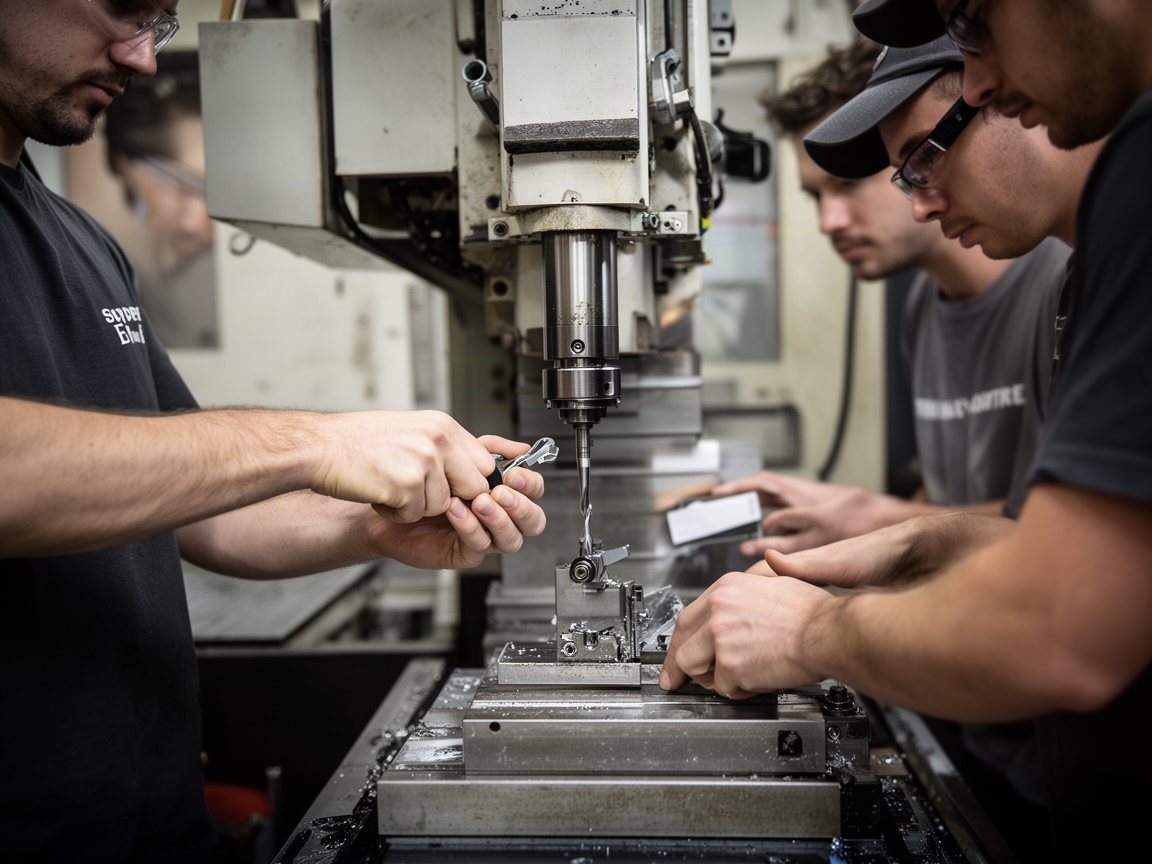
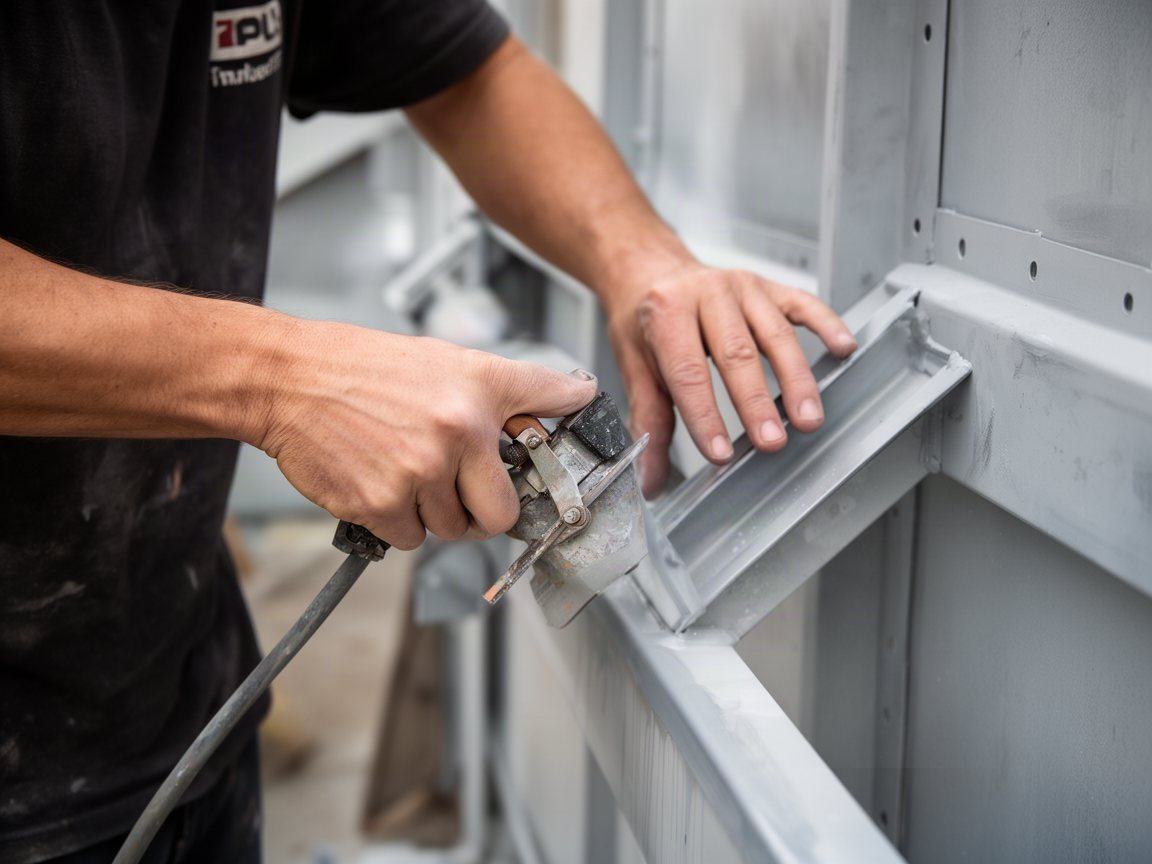
Deburring, graining, polishing, passivation of stainless, powder coating, wet painting, anodizing and plating through controlled processes with adhesion and coating thickness verification. Pre-treatment is where coating failures originate, so surface preparation is specified and controlled rather than assumed.
Request a Quote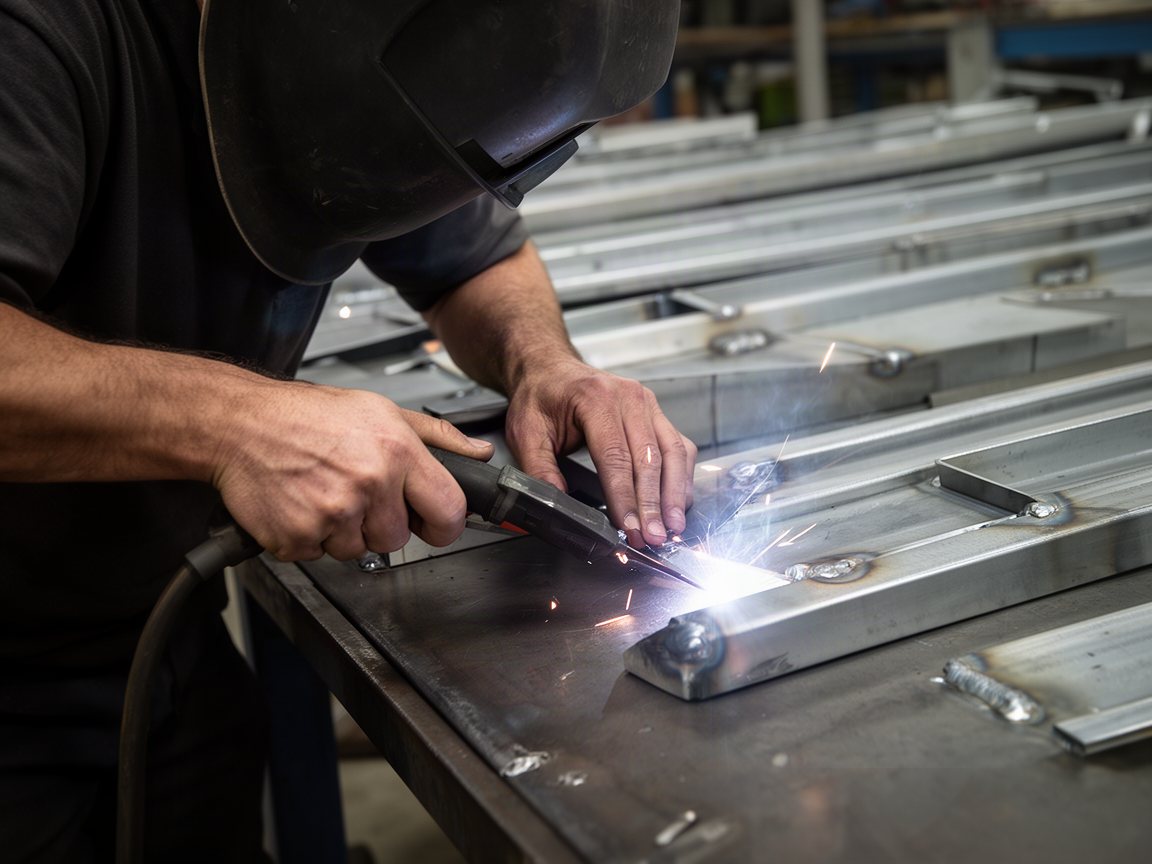
Prototype fabrication through to scheduled repeat production with documented setups, stored programs, fixturing retained and first-article inspection on new parts. Running both through the same shop means parts that worked as samples continue to work at volume.
Request a Quote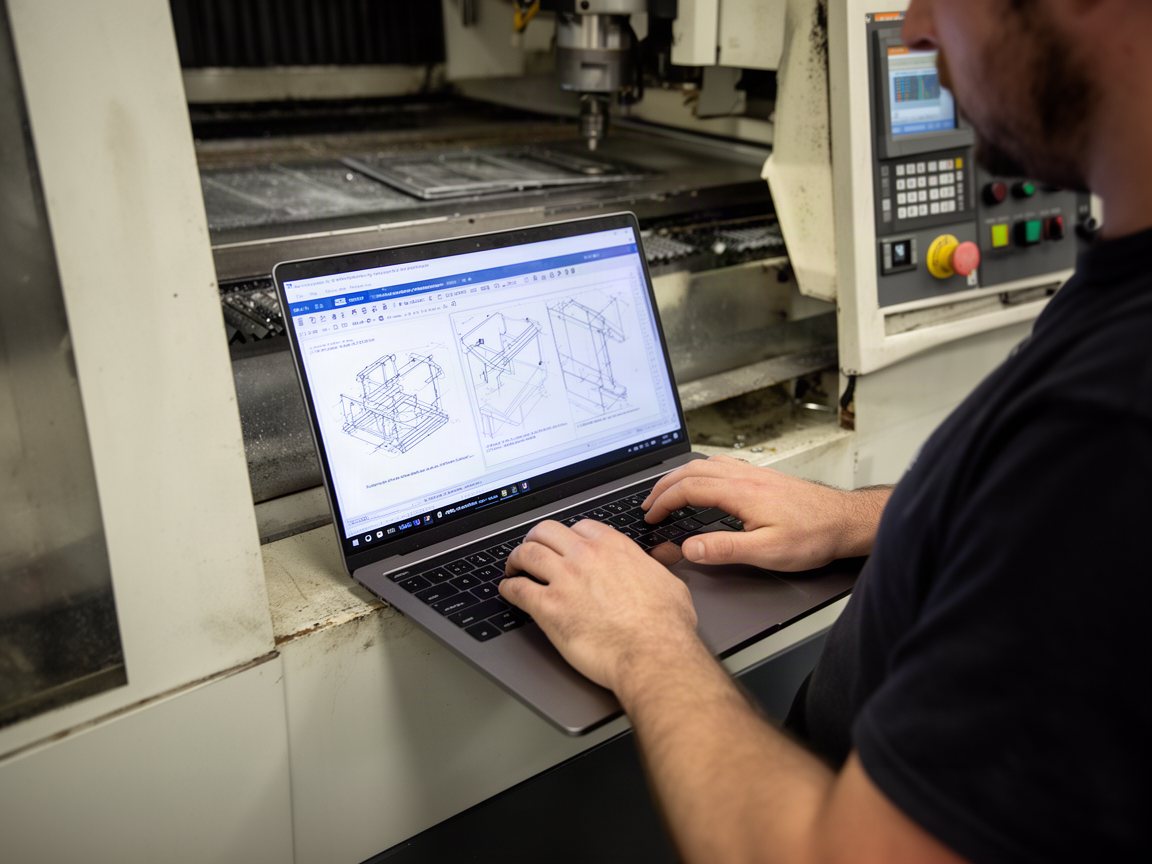
Precision forming on CNC press brakes with programmed bend sequences, tooling selected per material and radius, and springback allowance set for the specific alloy and temper. Bend sequence planning determines whether complex parts can be formed at all without collision.
Request a QuoteCompliance
Pre-treatment before coating is controlled and documented.
Our Process
Your drawings and models are reviewed for manufacturability, issues are raised with suggested alternatives, and the part is quoted with realistic tolerances stated.
Flat patterns, bend sequences and tooling are programmed, fixturing is prepared where needed, and a first article is produced and inspected against the drawing.
Parts are cut, formed, welded and hardware-inserted with distortion control, then finished and coated to specification with adhesion and thickness verified.
Assemblies are built up, functionally checked where applicable, inspected against the drawing with results recorded, then packed to protect finished surfaces.
MCB Smide & Maskin will review your parts for manufacturability, suggest alternatives where needed, and quote with realistic tolerances.
We deliver complete assemblies including welding, hardware insertion, finishing, powder coating and sub-assembly, so you receive parts ready to use rather than ready to process.
Projects & Case Studies
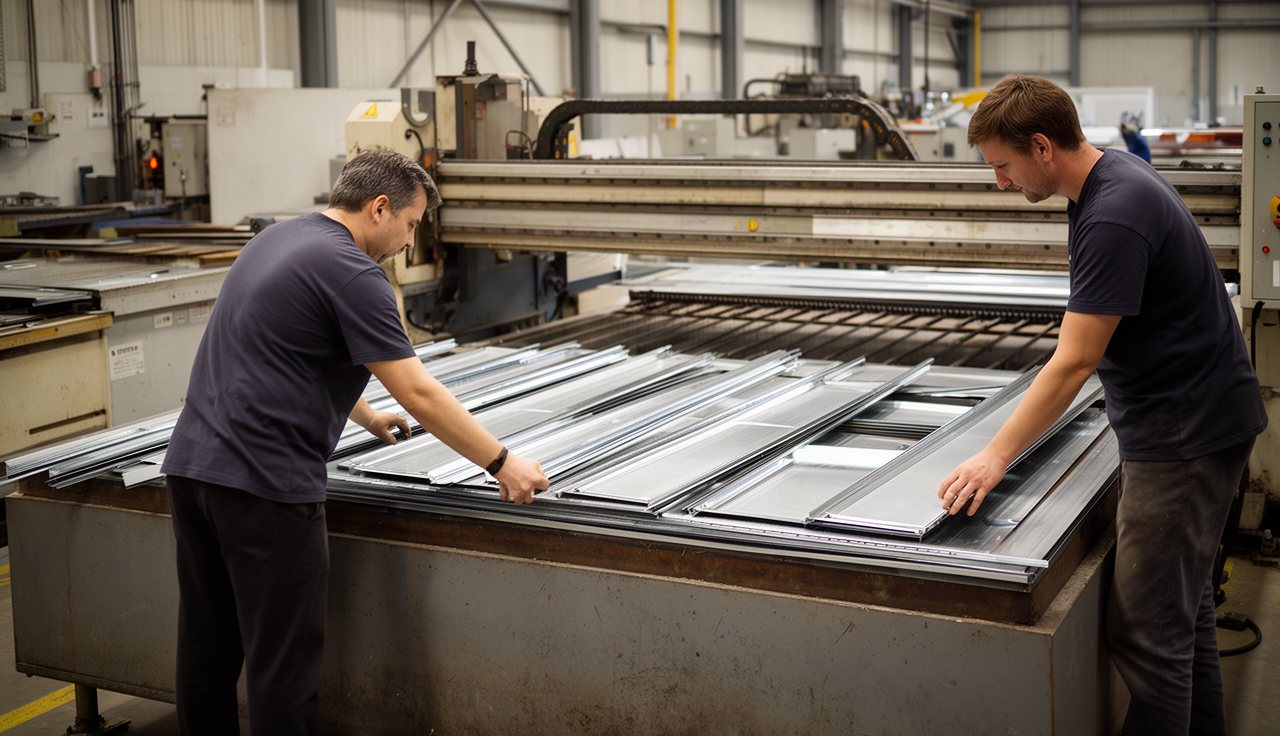
A range of electrical enclosures was taken from design review through production, with weld fixturing and sequence developed to control distortion so door and panel fit remained consistent across batches.
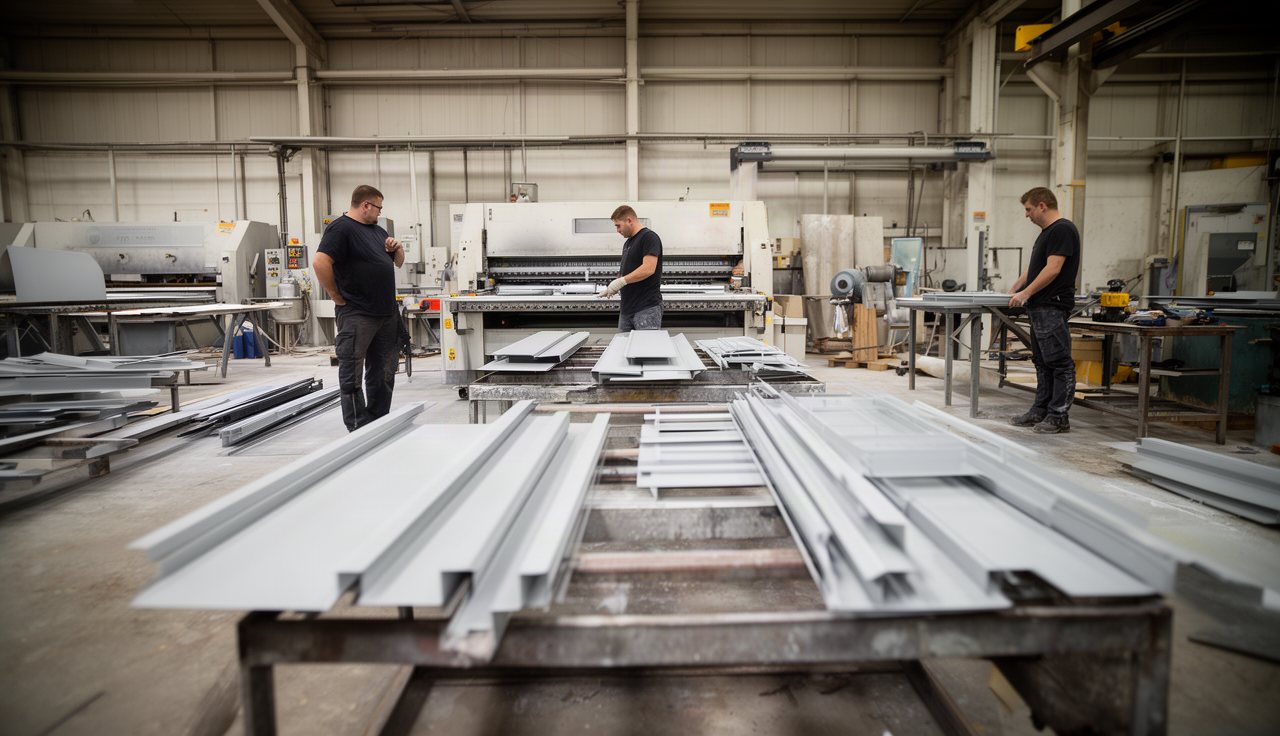
Recurring coating adhesion failures on a client\'s parts were traced to inadequate pre-treatment at their previous supplier. Controlled surface preparation with verification resolved the problem permanently.
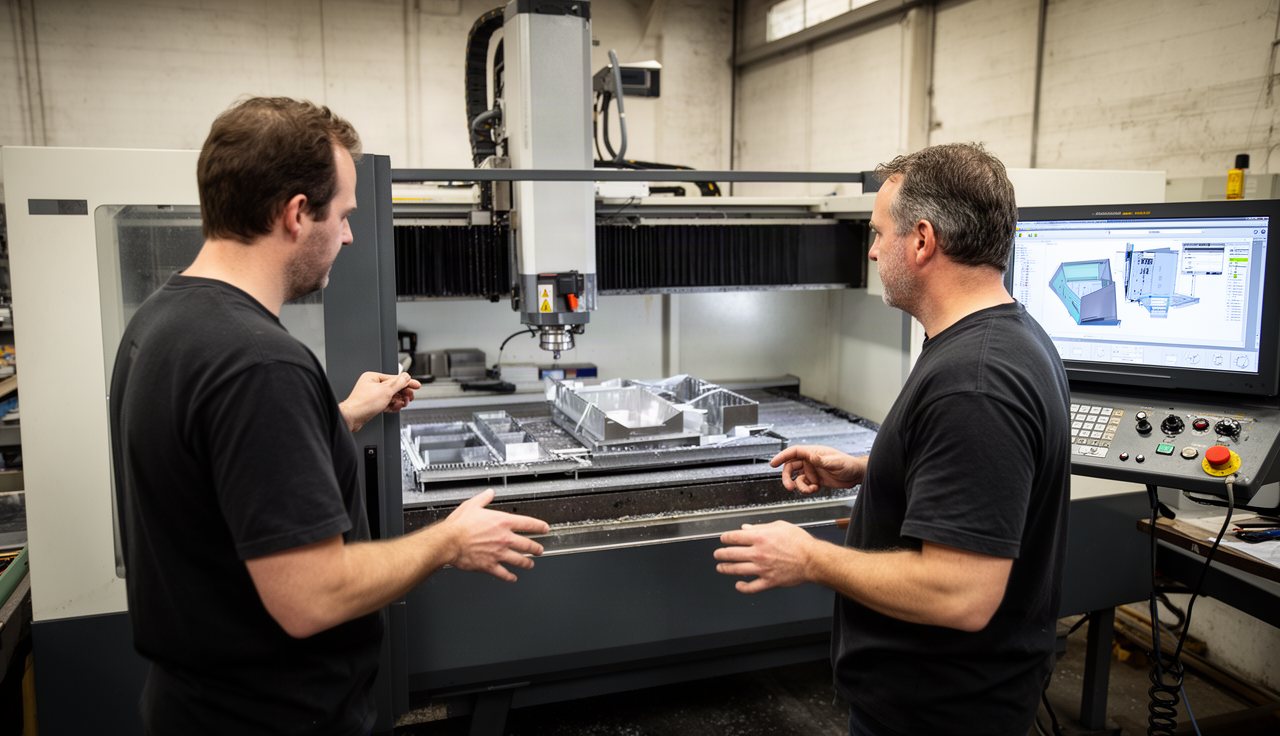
Stainless fabrications for food processing equipment were produced with controlled weld finishing, passivation and surface specification appropriate to hygienic cleaning requirements and documented for the client\'s compliance file.
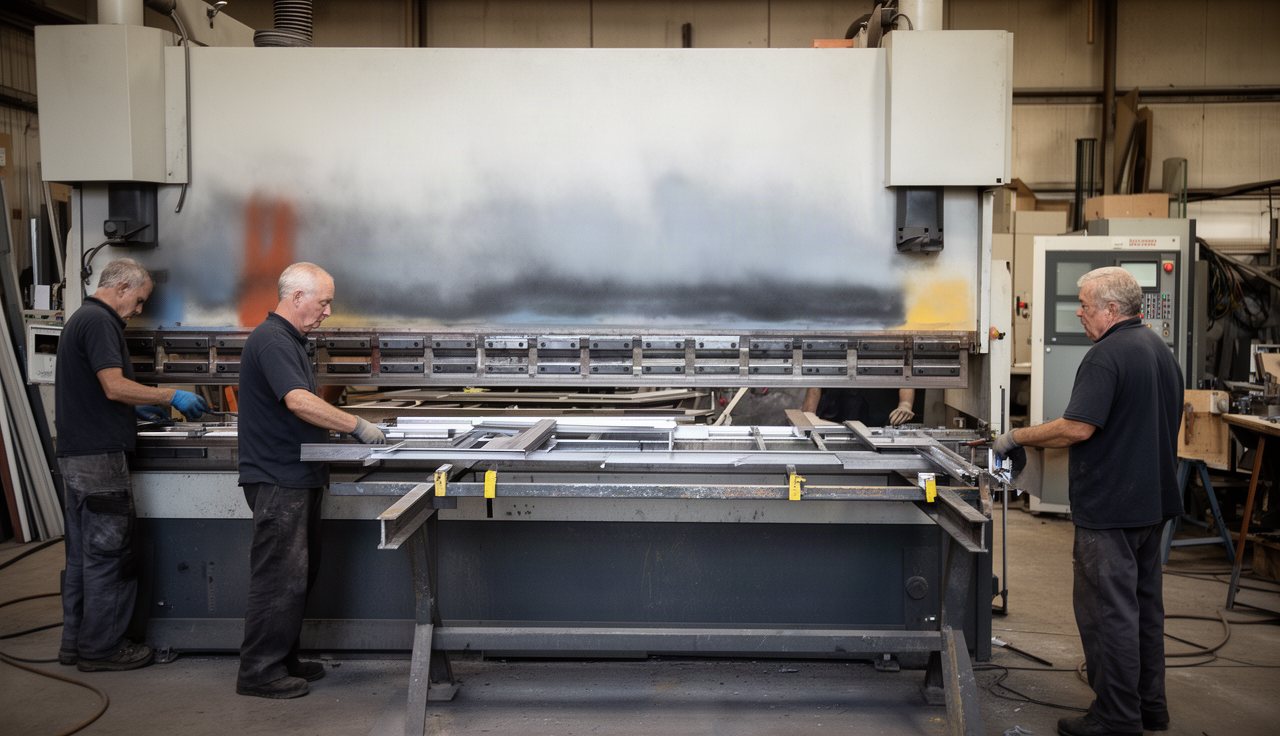
A bracket family was redesigned at quotation stage after review found flanges too short to form and holes too close to bend lines. The revised design cut secondary operations entirely.
Our Process
Your drawings and models are reviewed for manufacturability, issues are raised with suggested alternatives, and the part is quoted with realistic tolerances stated.
Flat patterns, bend sequences and tooling are programmed, fixturing is prepared where needed, and a first article is produced and inspected against the drawing.
Parts are cut, formed, welded and hardware-inserted with distortion control, then finished and coated to specification with adhesion and thickness verified.
Assemblies are built up, functionally checked where applicable, inspected against the drawing with results recorded, then packed to protect finished surfaces.
Track Record
MCB Smide & Maskin will review your parts for manufacturability, suggest alternatives where needed, and quote with realistic tolerances.
Urgent breakdown parts can often be cut and formed the same day.
Questions & Answers
Yes, including powder coating, plating, passivation, hardware insertion, gaskets, locks, labeling and functional checks. Delivering finished assemblies removes handling, transport and coordination steps that often cost more than the assembly labor they were meant to save.
Looser than machined parts, and dependent on material, thickness, feature count and the number of bends in a dimension chain. Tolerance accumulates across bends, so a dimension spanning several forms cannot hold a machining tolerance. We state what is achievable for your specific part.
Yes, and running both in the same shop is the point. Programs, tooling and fixturing developed for the prototype are documented and retained, so production parts reproduce the sample you approved rather than being reinterpreted by a different supplier.
Because most fabrication problems originate in the design, not the shop. Insufficient bend relief, flanges too short for the tooling, holes too close to bend lines and unachievable tolerance stacks are all cheap to fix at design stage and expensive to discover afterward.
Yes, both, with awareness of their differences. Aluminum springback and cracking behavior differ considerably from steel, and stainless requires attention to weld finishing, passivation and avoiding carbon contamination from shared tooling, which we manage through separation.
Almost always pre-treatment. Inadequate cleaning, degreasing or conversion coating produces adhesion failure regardless of the powder used. Surface preparation is where coating durability is decided, so we specify and verify it rather than treating it as a routine step.
Our Advantages
Programs, tooling and fixturing are stored, so repeat orders reproduce the part that was approved rather than a fresh interpretation of it.
Fixturing and weld sequence are planned for heat management, because distortion in a welded enclosure shows up immediately as door and panel misfit.
Hardware, gaskets, locks and labeling are fitted and checked, so you receive usable assemblies rather than parts needing further operations.
Bend relief, flange length, hole proximity and tolerance achievability are checked at quotation, with alternatives suggested rather than problems deferred.
Surface preparation is specified and verified, since almost every powder coating failure originates in pre-treatment rather than in the coating itself.
Forming allowance is set by alloy and temper, and we form test pieces on unfamiliar material instead of assuming a generic figure.
Bend allowances are calculated per material and thickness rather than dialed in by eye, which is what keeps formed parts within drawing tolerance.
Cleaning and pre-treatment stages before powder coating are process controlled and recorded, since adhesion failures are always a preparation failure.
We flag bend reliefs, tolerance stacks, hardware clearances and features that drive cost, so a small drawing change can save a great deal of money.
Urgent breakdown parts can often be cut and formed the same day.
Contact
Urgent breakdown parts can often be cut and formed the same day.
Sectors
Food equipment makers need hygienic welding and finishing to their own standards.
Last updated:
This Privacy Policy explains how MCB Smide & Maskin ("we", "us", "our") collects, uses, discloses and protects information when you visit galvetriona.com or contact us about our services. We keep data collection to what is necessary to answer inquiries and deliver contracted work.
Information you provide directly. When you submit an inquiry form, send an email or call us, we receive the details you choose to share: your name, organization, email address, telephone number, the service you are asking about and the content of your message.
Information collected automatically. Our web server records standard technical data for each request, including IP address, browser type and version, operating system, the pages requested, the date and time of the request and the referring page. This information is used for security monitoring, fault diagnosis and aggregate traffic statistics.
We do not knowingly collect special category data, financial account numbers or government identification numbers through this website, and we ask that you do not send such information through web forms or unencrypted email.
We use the information we collect to respond to your inquiry, prepare proposals and scopes of work, deliver and administer contracted services, maintain project and service records, meet legal, regulatory, insurance and procurement obligations, and protect the security and integrity of our systems.
We do not sell personal information. We do not use the information you provide for behavioral advertising, and we do not share it with advertising networks or data brokers.
Where data protection law requires a legal basis, we rely on: your consent, where you have voluntarily submitted an inquiry; the performance of a contract, where processing is necessary to quote, mobilize or deliver services; compliance with a legal obligation, including records retention, tax, safety and public procurement requirements; and our legitimate interests in operating, securing and improving our business, balanced against your rights.
We may share information with service providers who act on our instructions, such as email and hosting providers, and with subcontractors we engage where disclosure is necessary to deliver the service. These parties are permitted to use the information only for the purpose for which it was shared.
We may disclose information where required by law, court order, regulatory authority or a public client exercising audit rights under a contract, and where necessary to establish, exercise or defend legal claims.
Inquiry correspondence is retained for as long as needed to respond and for a reasonable period afterwards for business continuity. Project and contract records, including service logs, inspection records and photographic documentation, are retained for the period required by the contract, by applicable statute of limitations and by insurance and audit requirements, after which they are deleted or anonymized.
We apply administrative, technical and physical safeguards appropriate to the sensitivity of the information we hold, including transport encryption for this website, access controls on internal systems, role-based permissions and staff confidentiality obligations. No method of transmission or storage is completely secure, and we cannot guarantee absolute security.
Depending on where you live, you may have the right to request access to the personal information we hold about you, to request correction of inaccurate information, to request deletion, to object to or request restriction of certain processing, to request a copy in a portable format and to withdraw consent you previously gave.
To exercise any of these rights, write to support@galvetriona.com. We will respond within the timeframe required by applicable law and may need to verify your identity before acting on a request.
Our service providers may process data in countries other than the one in which you reside. Where personal information is transferred across borders, we rely on lawful transfer mechanisms and require appropriate contractual safeguards from the receiving party.
Our services are directed to organizations and property owners, not to children. We do not knowingly collect personal information from children. If you believe a child has provided us with personal information, contact support@galvetriona.com and we will delete it.
This website may link to third-party sites, such as standards bodies or regulatory resources. We are not responsible for the privacy practices or content of those sites, and we encourage you to review their policies before providing information.
We may update this Privacy Policy to reflect changes in our practices, technology or legal requirements. The revision date at the top of this page indicates when it was last changed. Material changes will be made evident on this page.
Questions, requests or complaints regarding this policy may be addressed to MCB Smide & Maskin, Signalgatan 6 B, 442 40 Kungälv, or by email to support@galvetriona.com. You may also have the right to lodge a complaint with your local data protection authority.
Last updated:
These Terms govern your use of galvetriona.com and describe the basis on which MCB Smide & Maskin provides information through this website. Separate written contracts govern any services we perform for you; nothing on this website creates a contract or an offer capable of acceptance.
By accessing or using this website you agree to these Terms. If you do not agree, please do not use the site. We may revise these Terms at any time by posting an updated version; your continued use after a revision constitutes acceptance of the revised Terms.
Descriptions of services, capabilities, standards, methods and past work are provided for general information. They are not technical specifications, engineering advice or a representation that a particular method is suitable for your site or your regulatory environment.
Capability, capacity and availability statements reflect our general practice and may change. Project figures and performance indicators are approximate and may be rounded or aggregated across contracts.
Submitting an inquiry through this website does not create a contract, reserve capacity or oblige either party to proceed. Services are performed only under a signed agreement, purchase order or awarded contract that sets out scope, specifications, schedule, price and terms. Where this website and a signed contract conflict, the contract governs.
You may view, download and print pages from this website for your own internal evaluation and procurement purposes. You may not copy, republish, sell, scrape, systematically extract or use automated means to access the site, nor use the site in any way that interferes with its operation or security, nor attempt to gain unauthorized access to any system or network connected to it.
All text, graphics, layout, photographs, illustrations, logos and other material on this website are owned by MCB Smide & Maskin or used with permission and are protected by applicable intellectual property laws. Trademarks, standards names and certification marks referenced on this site remain the property of their respective owners and are used for identification only.
Do not send confidential, proprietary or sensitive information through web forms. Information you submit through this website is not treated as confidential unless a confidentiality agreement is already in place between us, and we may use it to respond to and record your inquiry.
Links to third-party websites, standards and publications are provided for convenience. We do not control and are not responsible for the content, accuracy or availability of third-party material, and a link does not imply endorsement.
This website is provided on an "as is" and "as available" basis. To the fullest extent permitted by law, we disclaim all warranties, express or implied, including warranties of merchantability, fitness for a particular purpose, accuracy, non-infringement and uninterrupted or error-free operation.
To the fullest extent permitted by law, MCB Smide & Maskin will not be liable for any indirect, incidental, special, consequential or punitive damages, or for loss of profit, revenue, data or goodwill, arising out of or in connection with your use of this website, whether based in contract, tort, statute or otherwise. Nothing in these Terms limits liability that cannot lawfully be limited.
You agree to indemnify and hold harmless MCB Smide & Maskin and its personnel from claims, losses and expenses arising out of your misuse of this website or your breach of these Terms.
We aim to keep this website available but do not guarantee uninterrupted access. We may suspend, withdraw or restrict all or part of the site for maintenance, security or business reasons without notice.
These Terms are governed by the laws applicable at the principal place of business of MCB Smide & Maskin, without regard to conflict-of-law rules. If any provision is found unenforceable, the remaining provisions continue in full force.
Questions about these Terms may be sent to support@galvetriona.com or addressed to MCB Smide & Maskin, Signalgatan 6 B, 442 40 Kungälv.
Last updated:
This Cookie Policy explains how galvetriona.com uses cookies and similar local storage. We use the minimum necessary for the site to function and do not use advertising or cross-site tracking cookies.
Last updated:
The information on galvetriona.com is published by MCB Smide & Maskin for general informational purposes. It is not professional advice for any particular site, project or regulatory situation.
Content on this website does not constitute engineering, environmental, legal, safety, regulatory or financial advice, and must not be relied upon as a substitute for a site-specific assessment by a qualified professional engaged under contract. Conditions, codes and permitting requirements vary by jurisdiction and by site.
Descriptions of past work, performance indicators and outcomes describe what was achieved under the conditions of those specific contracts. They are not a prediction, promise or guarantee of results on any other project. Every scope, site and schedule is different.
We take reasonable care to keep this website accurate and current, but we make no representation or warranty that content is complete, correct or up to date. Standards, regulations, specifications and our own methods change over time, and the site may not reflect the most recent position.
Images, illustrations and diagrams on this website are illustrative and may be representative rather than photographs of a specific project. Statistics and project figures are approximate, may be rounded and may aggregate results across multiple contracts and years.
References to standards, codes, certifications or industry bodies are for identification and context. Such references do not imply endorsement by, affiliation with, or accreditation granted by those organizations beyond what is documented in the certificates we provide on request.
Links to other websites are provided for convenience only. We do not control third-party content and accept no responsibility for its accuracy, legality or availability. Inclusion of a link is not an endorsement.
To the fullest extent permitted by law, MCB Smide & Maskin accepts no liability for any loss or damage arising from reliance on information published on this website. Where we perform work for you, our obligations and liability are governed exclusively by the signed contract between us.
If you believe information on this site is inaccurate or out of date, please tell us at support@galvetriona.com so we can review it.
Last updated:
MCB Smide & Maskin is committed to making galvetriona.com usable by as many people as possible, including people who use assistive technology. This statement explains the measures we have taken and how to report a problem.
We aim to meet the Web Content Accessibility Guidelines (WCAG) 2.1 at Level AA as a target standard. Accessibility is treated as an ongoing obligation rather than a one-time project, and we review the site when we make significant changes to its structure or content.
Semantic HTML structure with a single main landmark, logical heading order and descriptive page titles, so screen reader users can navigate by structure.
A visible skip-to-content link, keyboard-operable navigation and menus, and focus styles that remain visible when navigating without a mouse.
Text and interface colors checked for contrast against their backgrounds, layouts that reflow at narrow widths and support browser text resizing without loss of content, and descriptive alternative text or accessible labels for images and icons that carry meaning.
Form fields with programmatically associated labels, required fields identified in text rather than by color alone, and link text that makes sense out of context.
Some decorative illustrations are presented without detailed descriptions because they convey no information beyond the surrounding text. Documents published in formats such as PDF may not meet the same standard as the website itself; we will provide an accessible alternative on request.
This website is designed to work with current versions of major browsers on desktop and mobile, used together with the assistive technologies available on those platforms. It may not perform as expected in browsers that are no longer supported by their vendor.
If you encounter a barrier on this website, or need information from it in an alternative format such as large print, plain text or a document read aloud, contact us at support@galvetriona.com or +46 303 365 151. Please tell us the page address and what you were trying to do so we can reproduce the problem.
We aim to acknowledge accessibility reports within five business days and will tell you what we intend to do and when. If an immediate fix is not possible, we will provide the information you needed by another means.
If you are not satisfied with our response, you may escalate the matter to the body responsible for accessibility enforcement in your jurisdiction. This statement is reviewed periodically and whenever the website undergoes substantial change.
Photographs on this website are used under open licenses that permit commercial use.
The following images are published under Creative Commons licenses and are listed with their original title and attribution as given by the source.
Prototype To Production
We deliver complete assemblies including welding, hardware insertion, finishing, powder coating and sub-assembly, so you receive parts ready to use rather than ready to process.
Drawings reviewed for manufacturability before anything is cut
Our Services
Laser cutting and CNC punching of blanks with forming features, louvers, embossments, countersinks and hardware preparation, nested for material yield. Punched forming features are often more economical than se
View DetailsInsertion of self-clinching nuts, studs and standoffs, plus tapping, counterboring, reaming and machining of fabricated parts where tolerance requires it. Hardware insertion is specified against sheet thickness
View DetailsWelding in mild steel, stainless and aluminum covering spot, stud, TIG and MIG processes, with fixturing to control distortion and weld sequences planned for heat management. Welded enclosures receive particula
View DetailsReview of new parts before quoting, covering bend relief, minimum flange length against available tooling, hole-to-bend proximity, tolerance achievability, nesting efficiency and weld distortion risk. Issues co
View DetailsSub-assembly and full assembly including hardware, gaskets, insulation, locks, hinges, labeling, wiring harness installation and functional checks, delivered ready to use. Taking assembly in-house removes handl
View DetailsDeburring, graining, polishing, passivation of stainless, powder coating, wet painting, anodizing and plating through controlled processes with adhesion and coating thickness verification. Pre-treatment is wher
View DetailsTrack Record
Our Advantages
Programs, tooling and fixturing are stored, so repeat orders reproduce the part that was approved rather than a fresh interpretation of it.
Fixturing and weld sequence are planned for heat management, because distortion in a welded enclosure shows up immediately as door and panel misfit.
Hardware, gaskets, locks and labeling are fitted and checked, so you receive usable assemblies rather than parts needing further operations.
Bend relief, flange length, hole proximity and tolerance achievability are checked at quotation, with alternatives suggested rather than problems deferred.
Surface preparation is specified and verified, since almost every powder coating failure originates in pre-treatment rather than in the coating itself.
Forming allowance is set by alloy and temper, and we form test pieces on unfamiliar material instead of assuming a generic figure.
Bend allowances are calculated per material and thickness rather than dialed in by eye, which is what keeps formed parts within drawing tolerance.
Cleaning and pre-treatment stages before powder coating are process controlled and recorded, since adhesion failures are always a preparation failure.
We flag bend reliefs, tolerance stacks, hardware clearances and features that drive cost, so a small drawing change can save a great deal of money.
Our Process
Your drawings and models are reviewed for manufacturability, issues are raised with suggested alternatives, and the part is quoted with realistic tolerances stated.
Flat patterns, bend sequences and tooling are programmed, fixturing is prepared where needed, and a first article is produced and inspected against the drawing.
Parts are cut, formed, welded and hardware-inserted with distortion control, then finished and coated to specification with adhesion and thickness verified.
Assemblies are built up, functionally checked where applicable, inspected against the drawing with results recorded, then packed to protect finished surfaces.
Projects & Case Studies
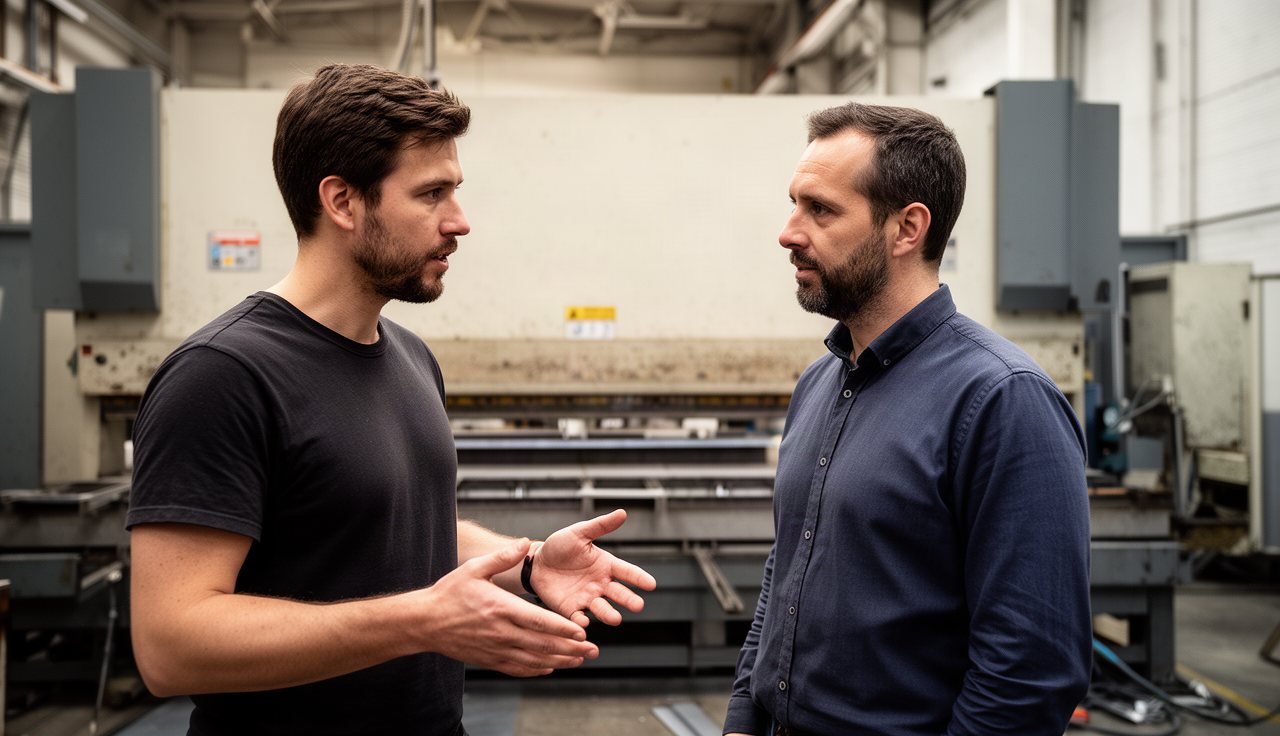 Enclosures
A range of electrical enclosures was taken from design review through production, with weld fixturing and sequence developed to control distortion so door and panel fit remained consistent across batches.
View Details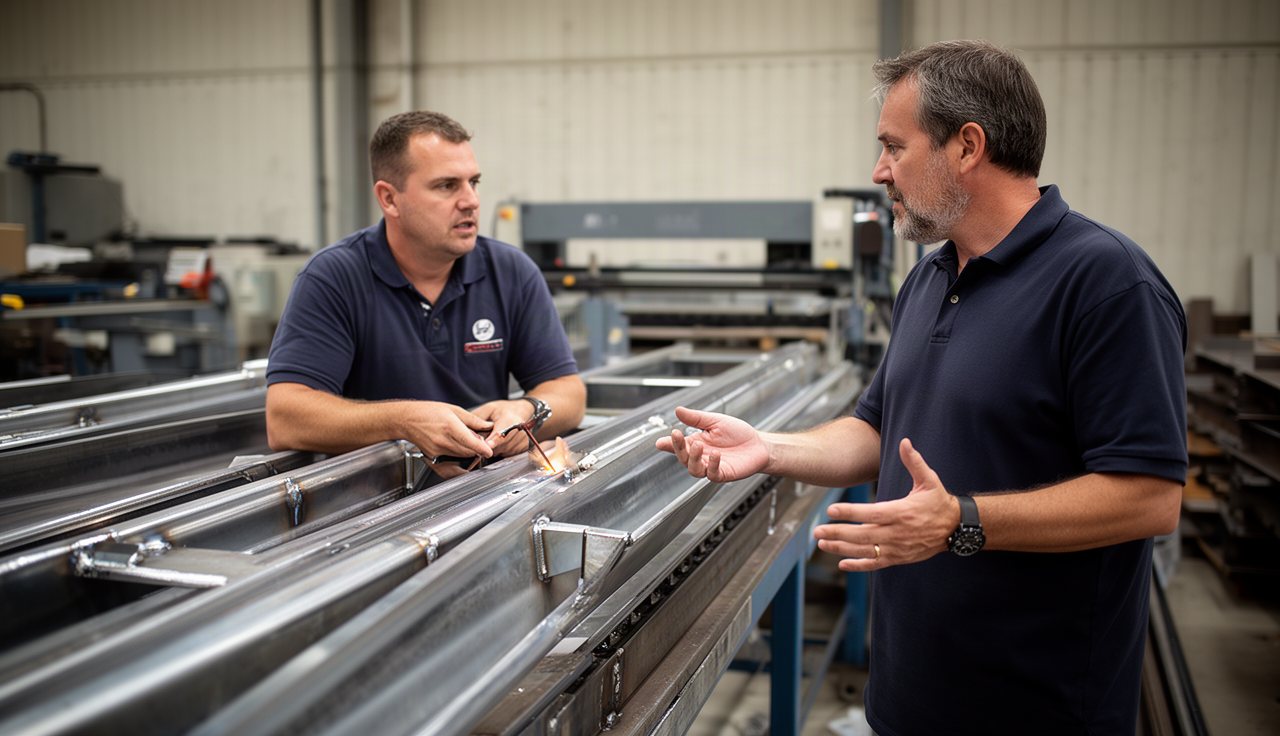 Finishing
Recurring coating adhesion failures on a client\'s parts were traced to inadequate pre-treatment at their previous supplier. Controlled surface preparation with verification resolved the problem permanently.
View Details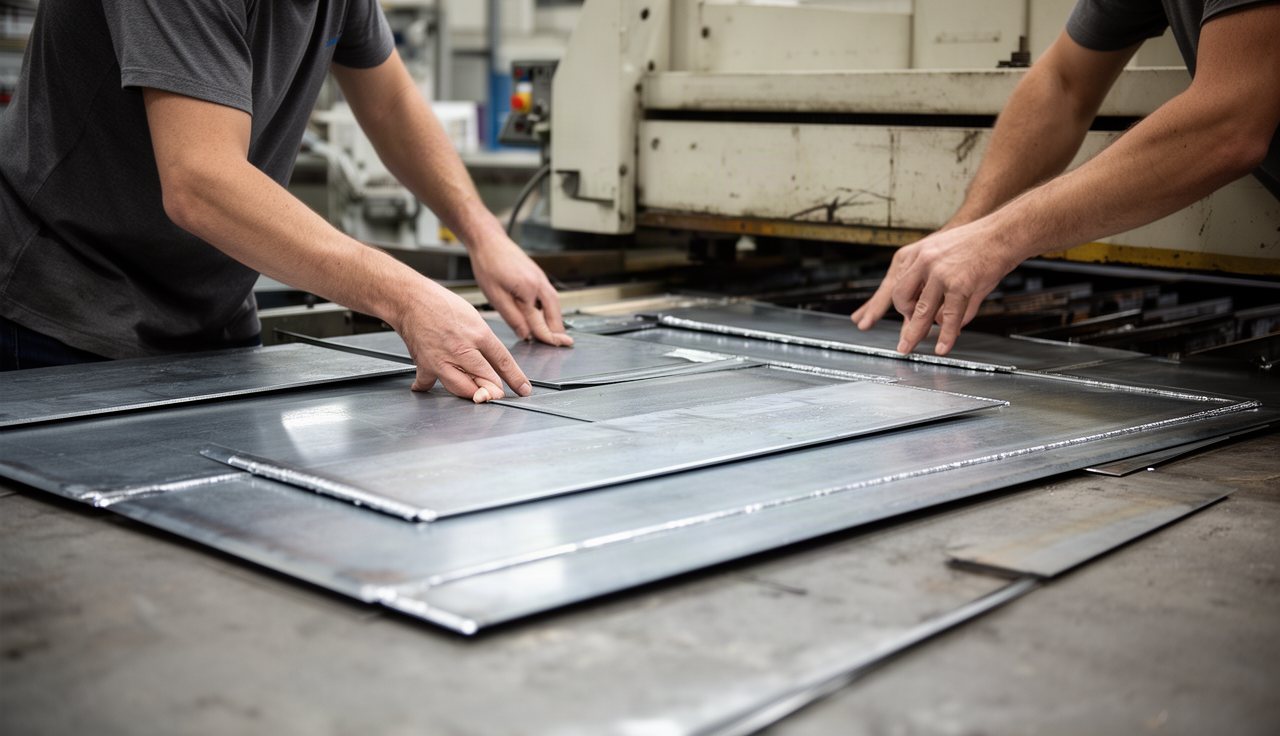 Stainless Work
Stainless fabrications for food processing equipment were produced with controlled weld finishing, passivation and surface specification appropriate to hygienic cleaning requirements and documented for the client\'s compliance file.
View Details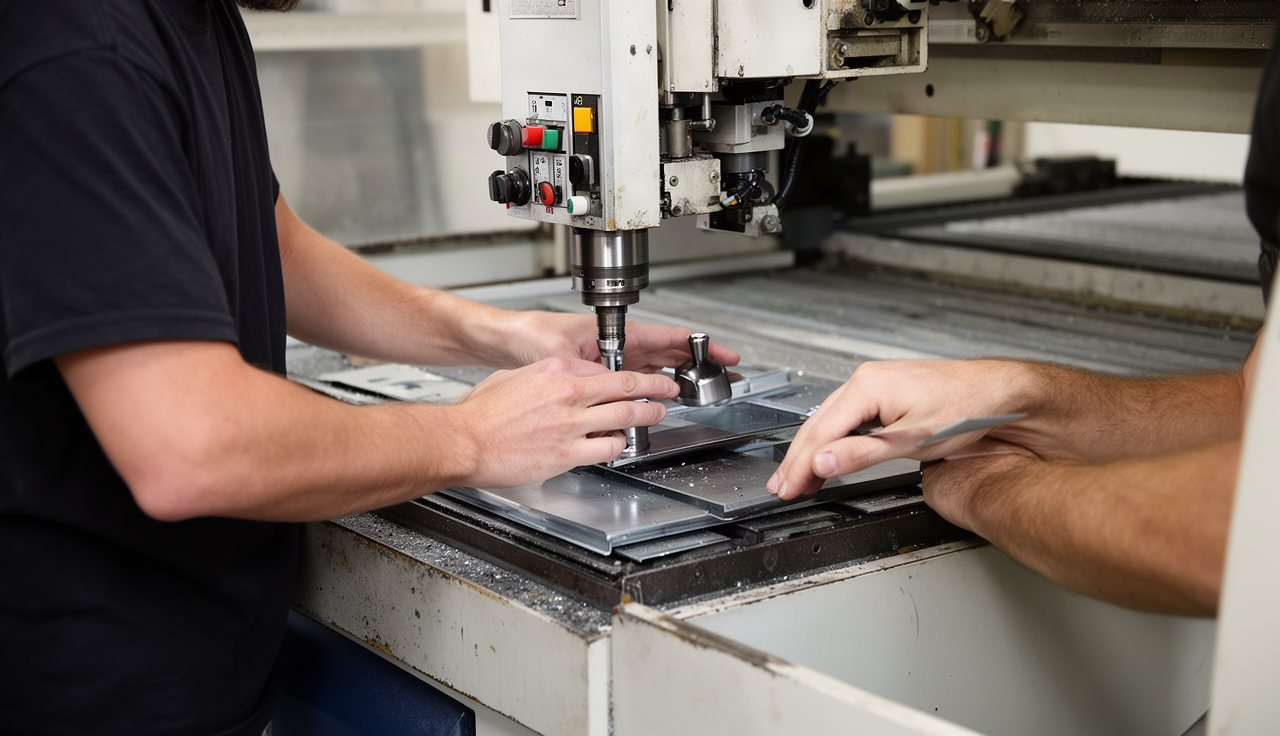 Design Review
A bracket family was redesigned at quotation stage after review found flanges too short to form and holes too close to bend lines. The revised design cut secondary operations entirely.
View DetailsFrom Our Desk
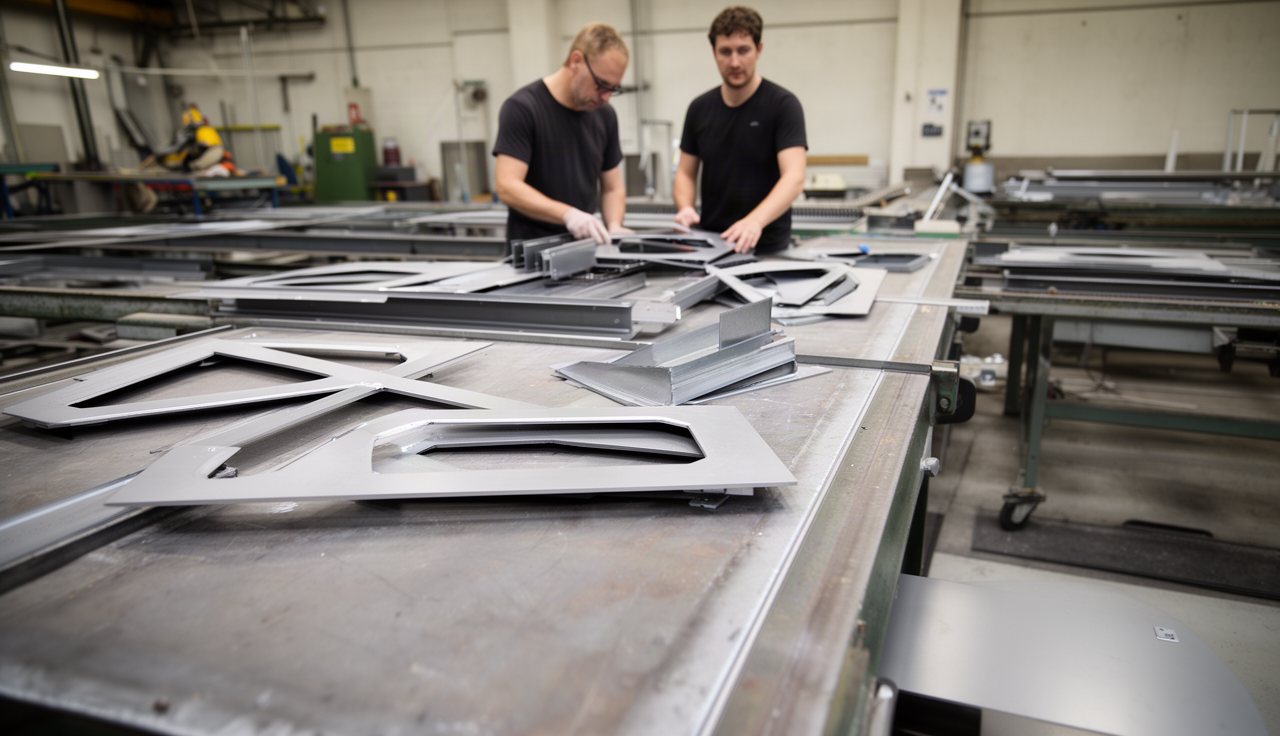
Powder is rarely the problem. What controlled cleaning, degreasing and conversion coating actually involves.
A dimension spanning several forms cannot hold a machining tolerance. How stacks should be dimensioned instead.
The most common sheet metal design omission, and the cheapest to fix before anything is cut.
Heat moves metal, and door fit shows it immediately. Why fixturing and weld sequence are planned, not improvised.
Client Feedback
Their design review changed four features before we committed. Two of those would have torn at the bend corners and we would have found out at first article.
The enclosure fit is consistent batch to batch, which it never was before. They explained it was weld fixturing and sequence, not the forming.
We had chased coating adhesion failures across two suppliers. They identified pre-treatment in the first conversation and it has not recurred since.
MCB Smide & Maskin will review your parts for manufacturability, suggest alternatives where needed, and quote with realistic tolerances.